Perundurai, Erode, TN, INDIA ISO 9001:2015 & ISO 14001:2015 Certified
Wastewater & Environmental

Zero Liquid Discharge (ZLD) Plants

Total water recovery systems integrating high-recovery Reverse Osmosis, Multi-Effect Evaporators (MEE), and crystallizers with zero effluent release.

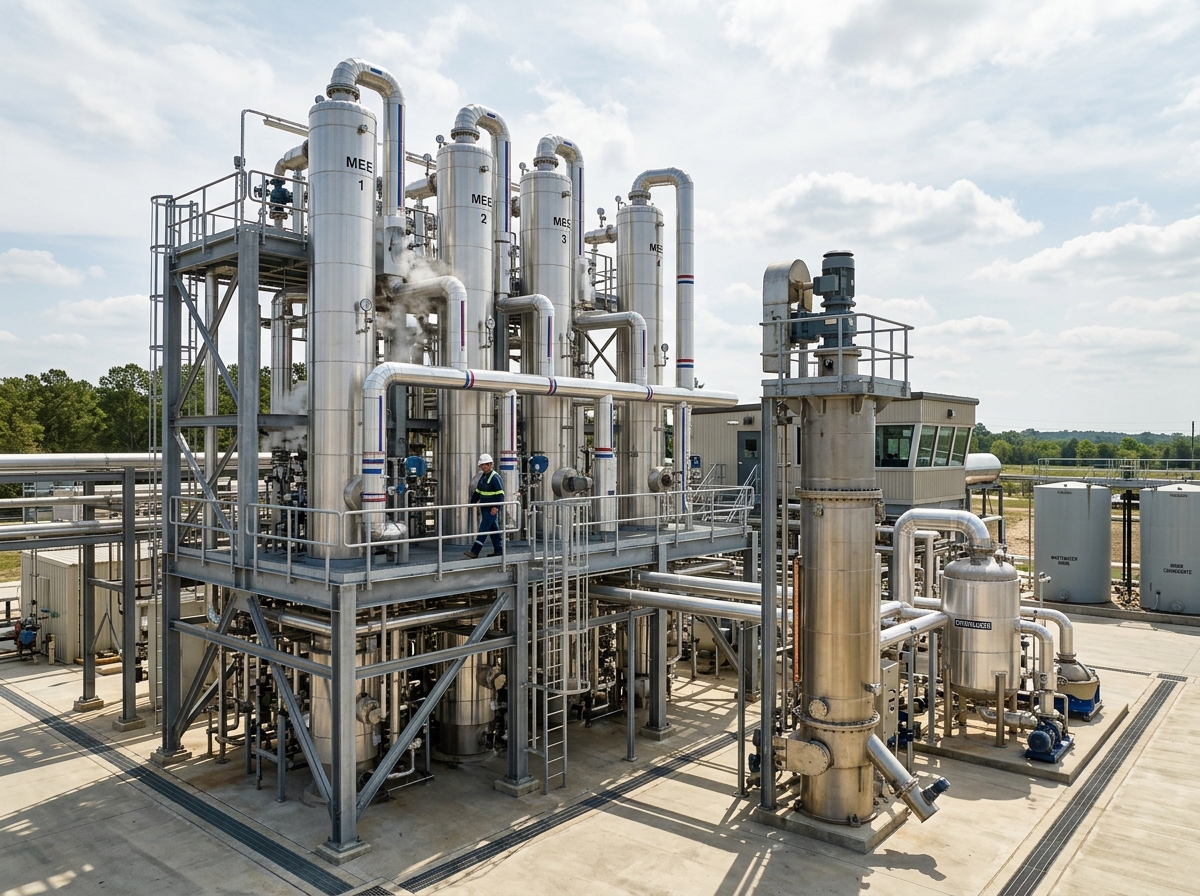
Zero Liquid Discharge (ZLD) Plants Primary View
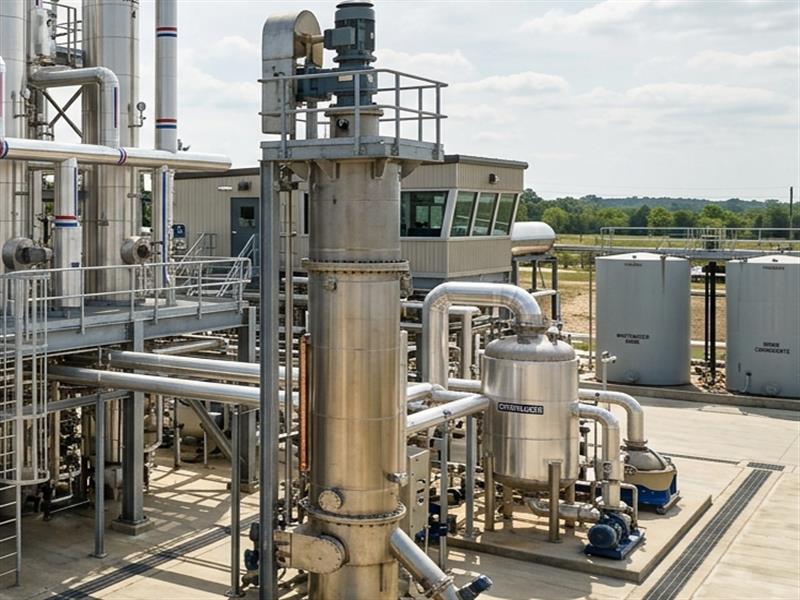
Zero Liquid Discharge (ZLD) Plants Operational Installation

Product Overview

Zero Liquid Discharge (ZLD) is the gold standard of sustainable industrial water stewardship. LiquidTeQ Engineering Corporation delivers comprehensive ZLD solutions that eliminate industrial wastewater discharge entirely. By combining high-pressure disc-tube reverse osmosis (DTRO), Multi-Effect Evaporators (MEE), Mechanical Vapor Recompression (MVR), and Agitated Thin Film Dryers (ATFD), our plants recover 95% to 99% of wastewater as pure distilled water while converting remaining salts into dry, solid crystals for safe disposal or industrial reuse.

Key Engineering Features

High-recovery multi-stage RO skids concentrating brine up to 70,000-100,000 ppm TDS
Energy-efficient Falling Film or Forced Circulation Multi-Effect Evaporators (MEE)
Mechanical Vapor Recompression (MVR) technology slashing thermal steam demand
Agitated Thin Film Dryer (ATFD) producing dry crystallized salt powder
Condensate polishing unit (CPU) recycling clean vapor distillate back into boiler or process
Fabricated in high-alloy metallurgy: SS316L, Duplex 2205, or Titanium Grade 2

Technical Specifications

Standard engineering design parameters (custom engineered values available upon request):

Parameter / Specification Design Value / Standard Metric
Overall Water Recovery 95% to 99% recovered as pure distilled water
Distillate Water Quality TDS < 50 ppm, suitable for boiler make-up or process
Brine Concentration Concentrated to 300,000+ ppm TDS before crystallization
Evaporator Configuration Triple/Quadruple Effect with Thermo-Compressor (TVR/MVR)
Dryer Type Vertical Agitated Thin Film Dryer (ATFD) with scrapers
Capacities 5 KLD to 1,000+ KLD effluent evaporation systems

Applications & Industries Served

Textile processing clusters in sensitive river basins (e.g., Bhavani/Cauvery river zones)
Distilleries, breweries, and ethanol fermentation industries
Specialty chemical and pharmaceutical bulk drug manufacturing parks
Tanneries, leather processing, and electroplating complexes

Operational Benefits & Advantages

01.
100% immunity from environmental shutdown notices and pollution penalties
02.
Secures water independence during municipal dry seasons and ground water scarcity
03.
Recovers sellable sodium chloride / sodium sulfate salt by-products
04.
Lowest specific steam and electrical energy consumption per kiloliter evaporated

Frequently Asked Questions

Yes. By recovering over 95% of fresh water on-site, the plant dramatically slashes daily tanker water purchasing costs. Furthermore, our energy-efficient MEE and MVR designs reduce thermal operating costs by up to 40% compared to legacy evaporators.

Contact Engineering Specialist

Looking for the Right Engineering Solution?

Consult with our experienced chemical and environmental engineers for customized water treatment, DEF dispensing, or Zero Liquid Discharge plants.